Related Gas Detector
|
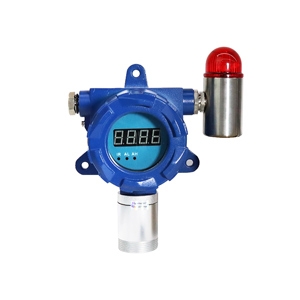
Model |
GD300-SO2 |
|
Gas |
Sulfur Dioxide (SO2) |
| Range | 0 to 1ppm, 0 to 5ppm, 0 to 10ppm, 0 to 20ppm, 0 to 50ppm, 0 to 100ppm, 0 to 500ppm, 0 to 1000ppm |
| Resolution | 0.001ppm(0-1/5ppm), 0.01ppm (0-10/20/50ppm), 0.1ppm (0-100ppm), 1ppm (0-500/1000ppm) |
| Accuracy | ≤±3% F.S. |
| Explosion-proof Grade | II 2G Ex ia IIC T4 Ga |
| Certification | CE, ATEX |
Case Study: Online SO2 Detection for Steel Desulfurization Process
Sulfur Dioxide (SO2) monitoring plays an important role in steel manufacturing, especially during desulfurization and combustion-related processes. Effective SO2 detection helps companies control emissions, improve environmental management, and maintain stable production conditions. This case study describes how a stainless steel manufacturer implemented an online SO2 monitoring solution at the hot blast furnace desulfurization inlet to achieve reliable gas measurement in a challenging industrial environment.
Challenge
As a leading stainless steel manufacturer, the customer was committed to developing a green and intelligent manufacturing facility with high production efficiency and strict environmental management standards.
During the steel production process, sulfur-containing materials can generate Sulfur Dioxide (SO2), which is one of the major harmful gases requiring monitoring and control. To improve emission management, the engineering contractor was required to install an online SO2 monitoring device at the desulfurization inlet of the hot blast furnace.
However, the application environment presented several challenges:
- The gas pipeline was installed outdoors and exposed to harsh industrial conditions.
- Gas samples contained dust, impurities, and moisture from the desulfurization process.
- Gas temperature could reach up to 200°C under certain operating conditions.
- A complete CEMS (Continuous Emission Monitoring System) was considered unnecessary due to the relatively moderate monitoring requirements.
The customer needed a reliable SO2 detection solution that could provide continuous monitoring while reducing system complexity and maintenance costs.
Solution
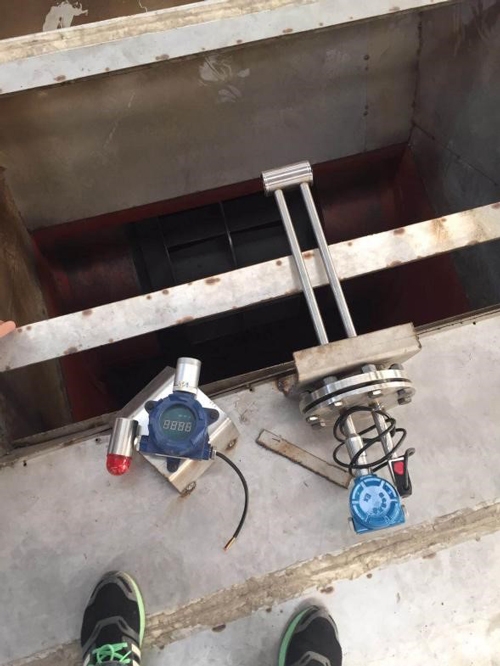
After evaluating the customer's requirements and the site conditions, GasDog recommended a fixed SO2 gas monitoring system designed for industrial pipeline applications. The system was configured with a GD300-SO2 fixed SO2 detector and sampling pretreatment components to ensure stable measurement performance in the desulfurization environment.
The solution included:
- 4-20mA analog output and RS485 communication for easy integration with existing monitoring systems.
- Dual flowmeter design to regulate both positive and negative pressure gas flow, improving sampling stability and measurement consistency.
- Optional filtration and protection components, including solenoid valves, stainless steel filters, oil removal units, dust removal devices, dryers, and dehumidifiers, helping protect the sensor from contaminants.
- High-temperature sampling probe rated up to 600°C, which reduces sample gas temperature and removes moisture before measurement to improve detection accuracy.
The complete sampling and pretreatment system was designed for simple installation. After mounting and power connection, the system can operate continuously for 24/7 SO2 monitoring with minimal daily operation requirements.
Result
The online SO2 detection solution provided the steel manufacturer with a reliable method for continuous emission monitoring at the hot blast furnace desulfurization inlet. The system enabled the customer to obtain real-time SO2 concentration data during production, improve control over desulfurization process conditions, reduce the impact of dust, moisture, and temperature fluctuations on measurement accuracy, and avoid the higher cost and complexity associated with a full CEMS installation. By combining stable gas sampling, reliable signal communication, and effective protective pretreatment components, the monitoring system achieved dependable long-term operation in a demanding industrial environment.
Key Takeaway
For steel plants and other heavy industries, SO2 monitoring in high-temperature and dusty environments requires more than just a gas sensor. A complete solution combining fixed detection, sampling pretreatment, and communication capabilities can provide accurate and continuous monitoring while keeping installation and maintenance costs under control.
This case demonstrates that a customized online SO2 monitoring system can effectively support environmental compliance, process optimization, and safer industrial operations.
Looking for a SO2 gas detection solution? Contact GasDog to discuss your application and find the right portable or fixed gas detection solution.


